Key takeaways
- Recesses, inside corners and channels resist electrostatic deposition because powder builds at the opening.
- Circle critical recesses on the drawing and state whether coverage there is cosmetic, protective or functional.
- Verify coverage on a representative first article; a flat panel cannot prove coverage inside a deep channel.
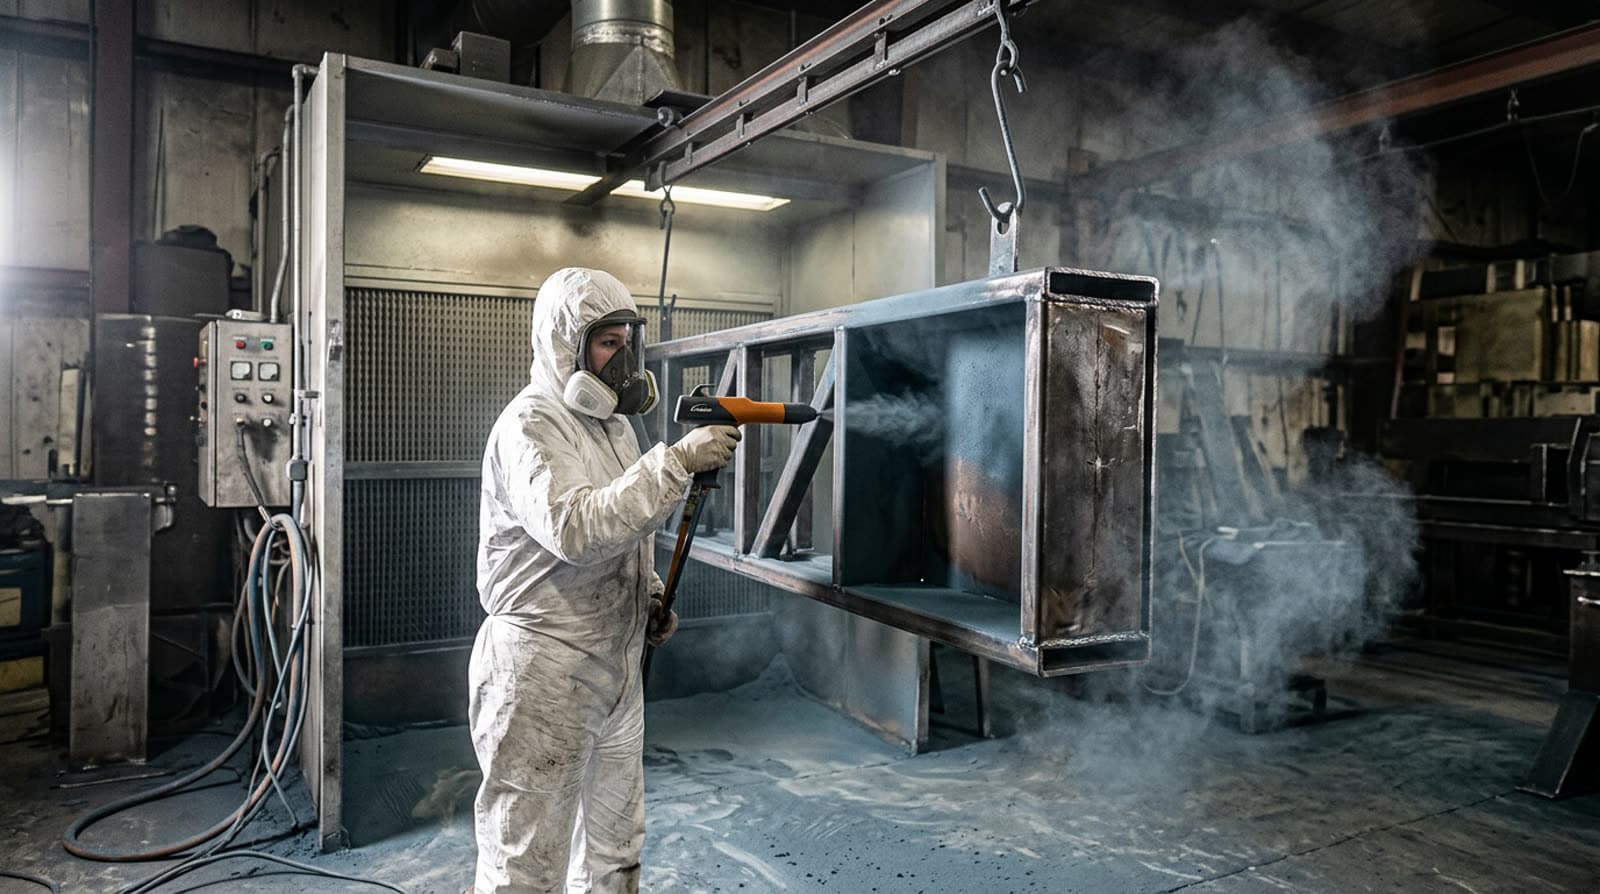
A complex metal part can look evenly coated on its broad faces while powder coverage is weak inside a recess. The electrostatic field and part geometry affect deposition, so the design and inspection plan need to name those areas.
Why recesses are difficult
The Powder Coating Institute describes Faraday areas as recesses, inside corners, channels and similar features where the external electric field encourages powder to deposit at the opening. Airflow, charging and field settings influence whether powder reaches the interior. More passes over the opening do not necessarily solve the problem and may overbuild its edges.
Deep blind pockets and enclosed cavities should never be assumed to have complete electrostatic coverage. Discuss them during design review.
- Deep channels and inside corners
- Closely spaced fins or brackets
- Box sections and blind pockets
Make hard-to-reach areas visible in the RFQ
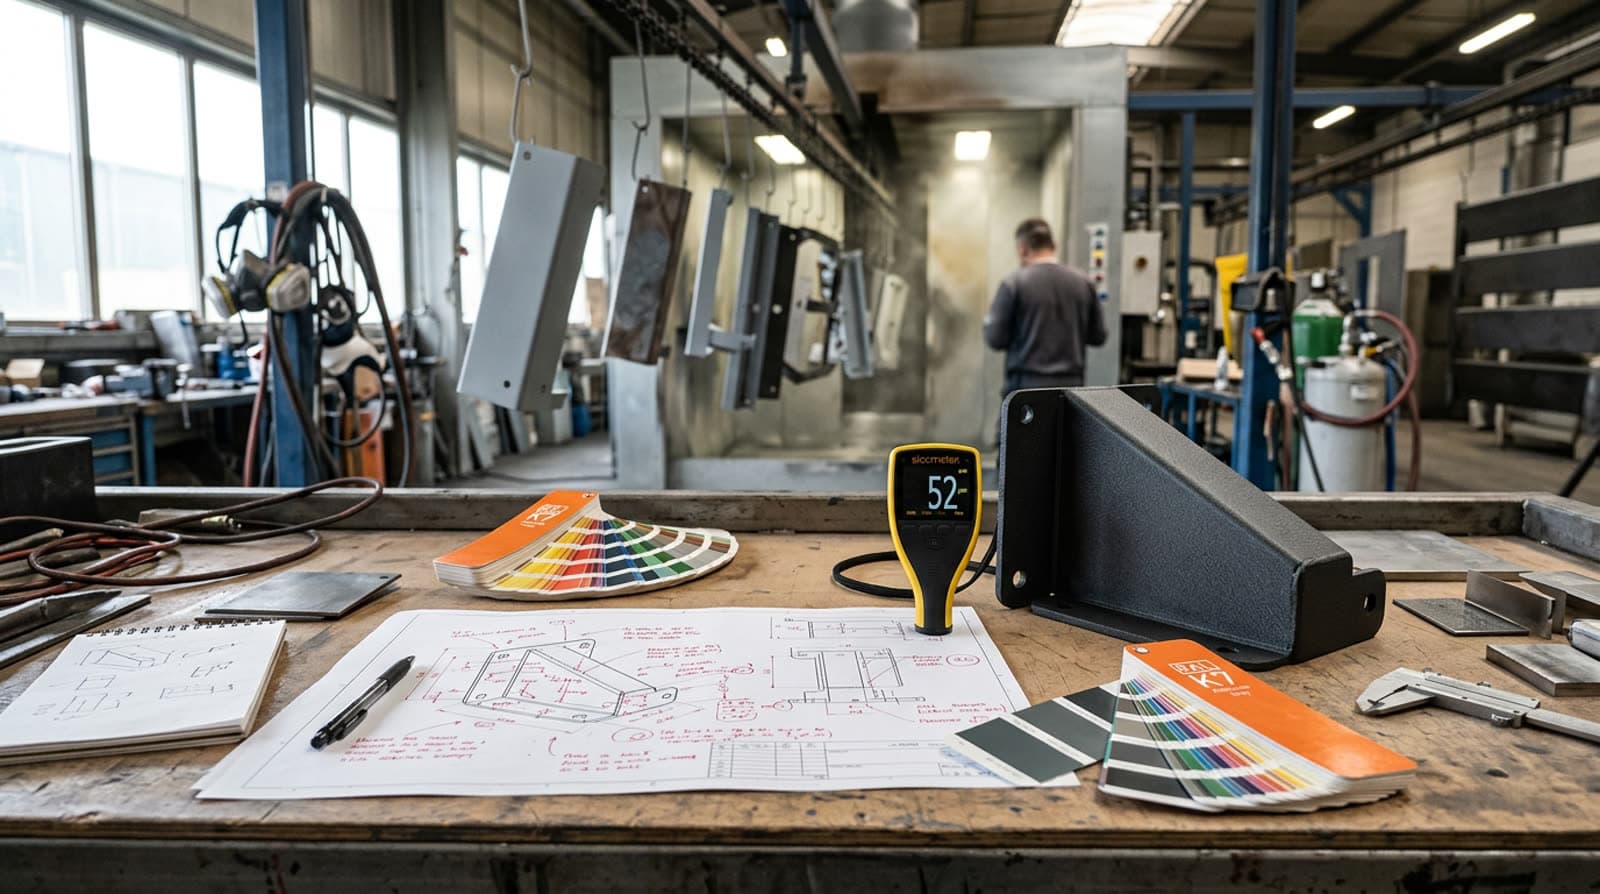
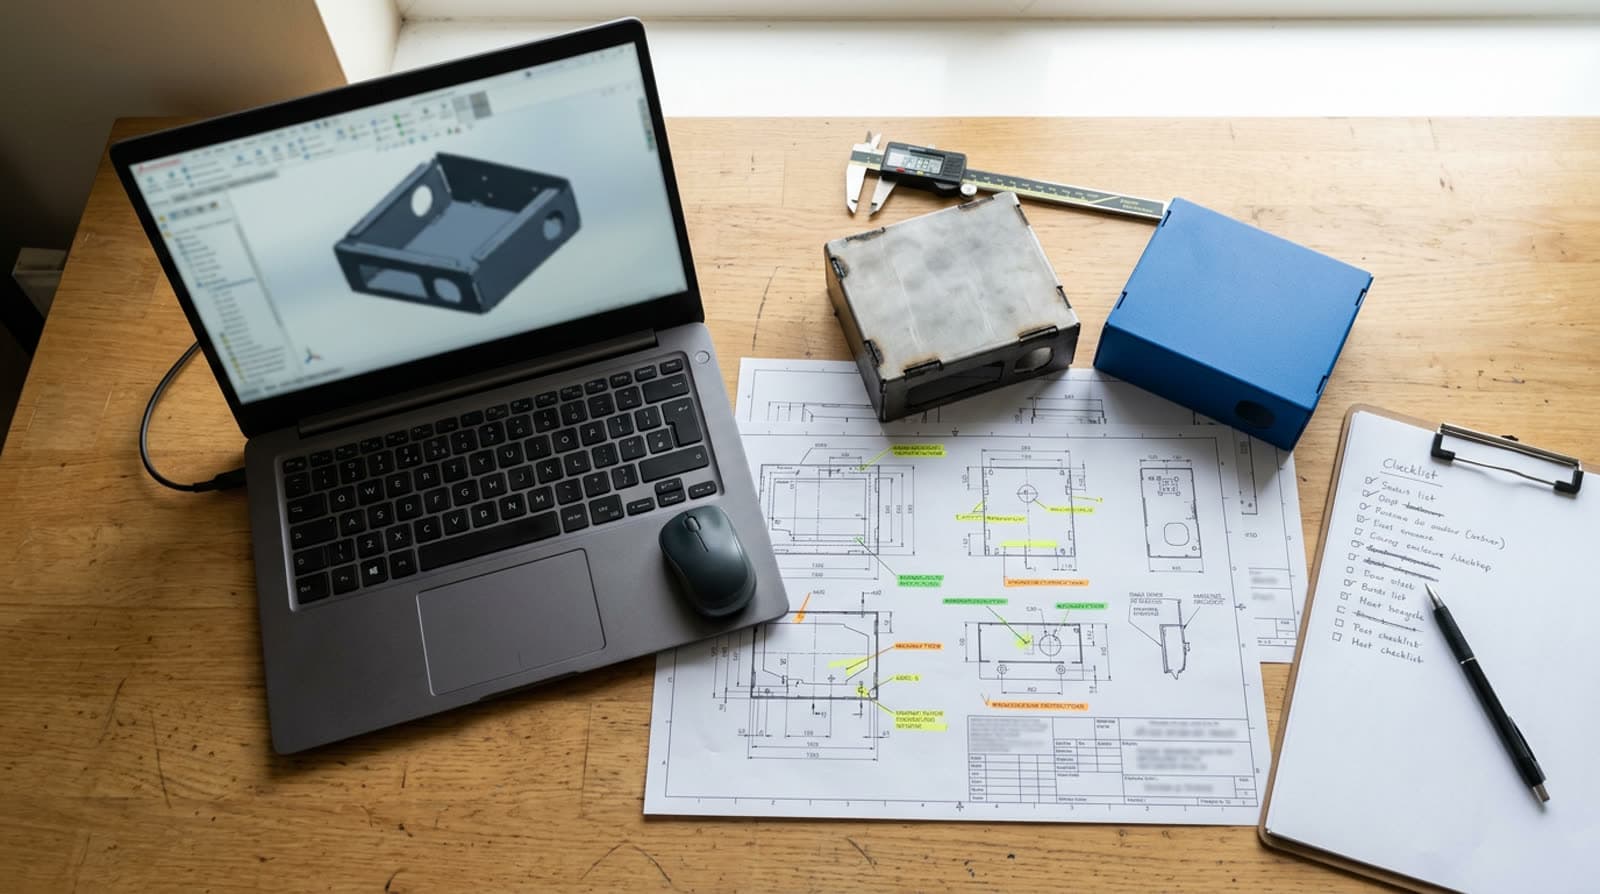
Circle critical recesses on the drawing and explain whether the coating is cosmetic, corrosion protective or functional there. Ask the coater to assess spray access, part orientation and whether the chosen method can meet the acceptance requirement. Changes to geometry or assembly order may be more effective than changing a spray setting.
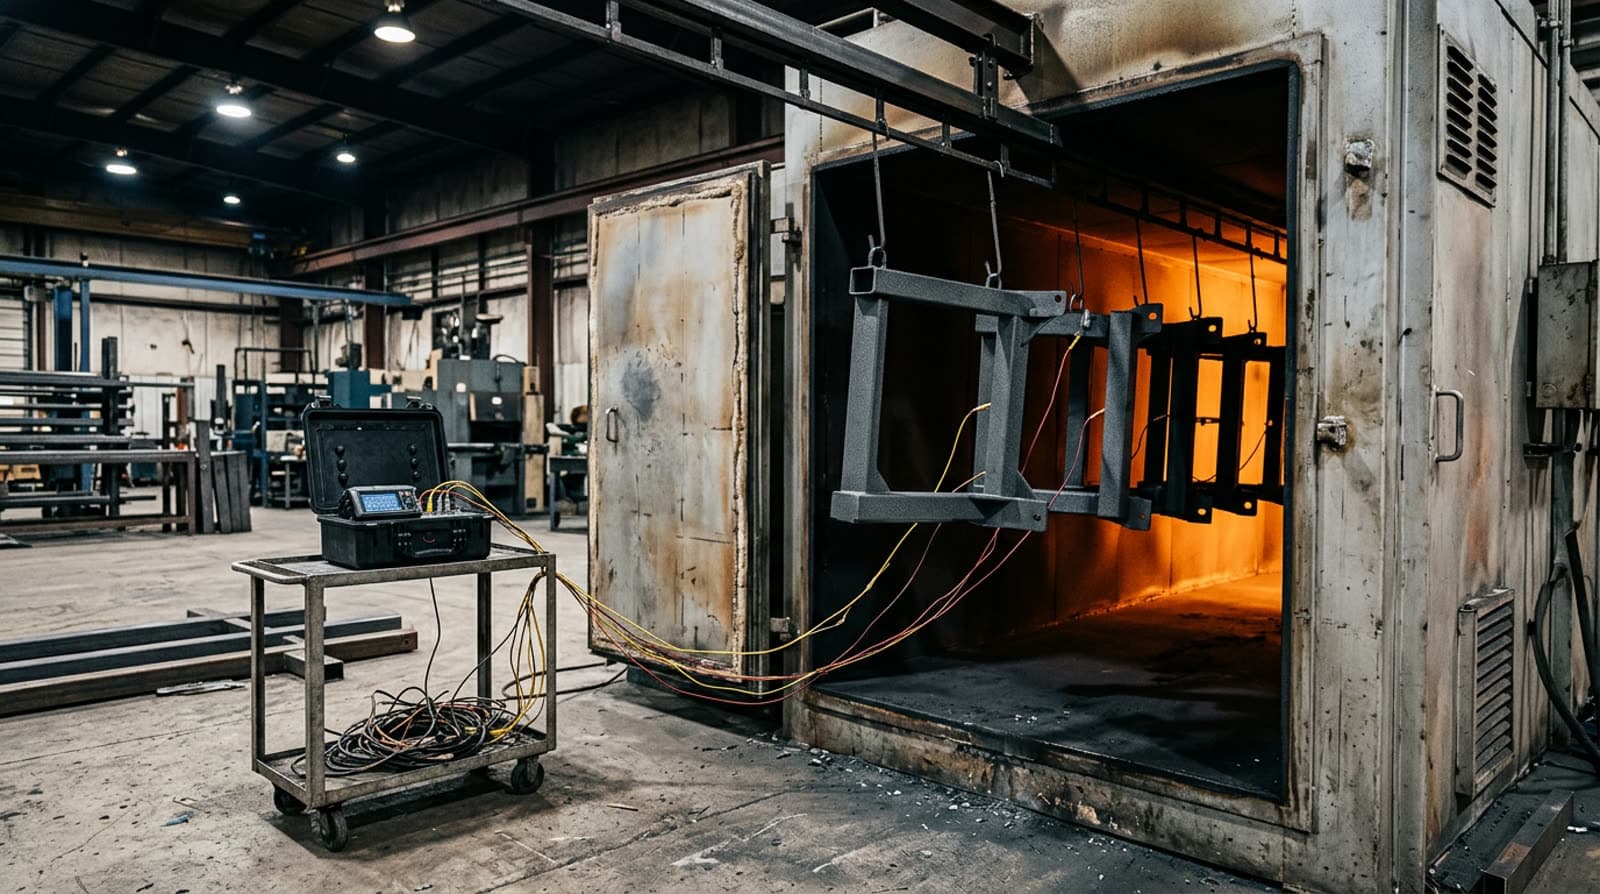
Use a representative first article with the same geometry, preparation and coating system. Inspect the recess and outer edge separately, including thickness where a suitable gauge can reach.
A flat panel result cannot demonstrate coverage in a deep fabricated channel.
Decide before approving production
If the required coverage cannot be verified, revisit the part design, a different application route or a revised protection plan with the engineer. Record permitted touch-up and inaccessible surfaces explicitly; ambiguity discovered after finishing is expensive.
Frequently asked questions
What is the Faraday cage effect in powder coating?
It is the tendency of the external electric field to deposit powder at the opening of recesses, inside corners and channels, leaving the interior with weak coverage.
Can more spray passes fix Faraday cage areas?
Not necessarily. Extra passes may overbuild the edges of the opening. Part orientation, spray access, geometry changes or a different application route may be more effective.
How do you confirm coverage in a recess?
Coat a representative first article with the same geometry, preparation and system, then inspect the recess and outer edge separately, measuring thickness where a gauge can reach.
Next step
Worried about coverage inside a complex part?
Send the drawing with the hard-to-reach areas circled. We will assess spray access and orientation before you commit to production.
- ISO 9001:2015 registered
- Technical review before pricing
- Toronto facility, North American service