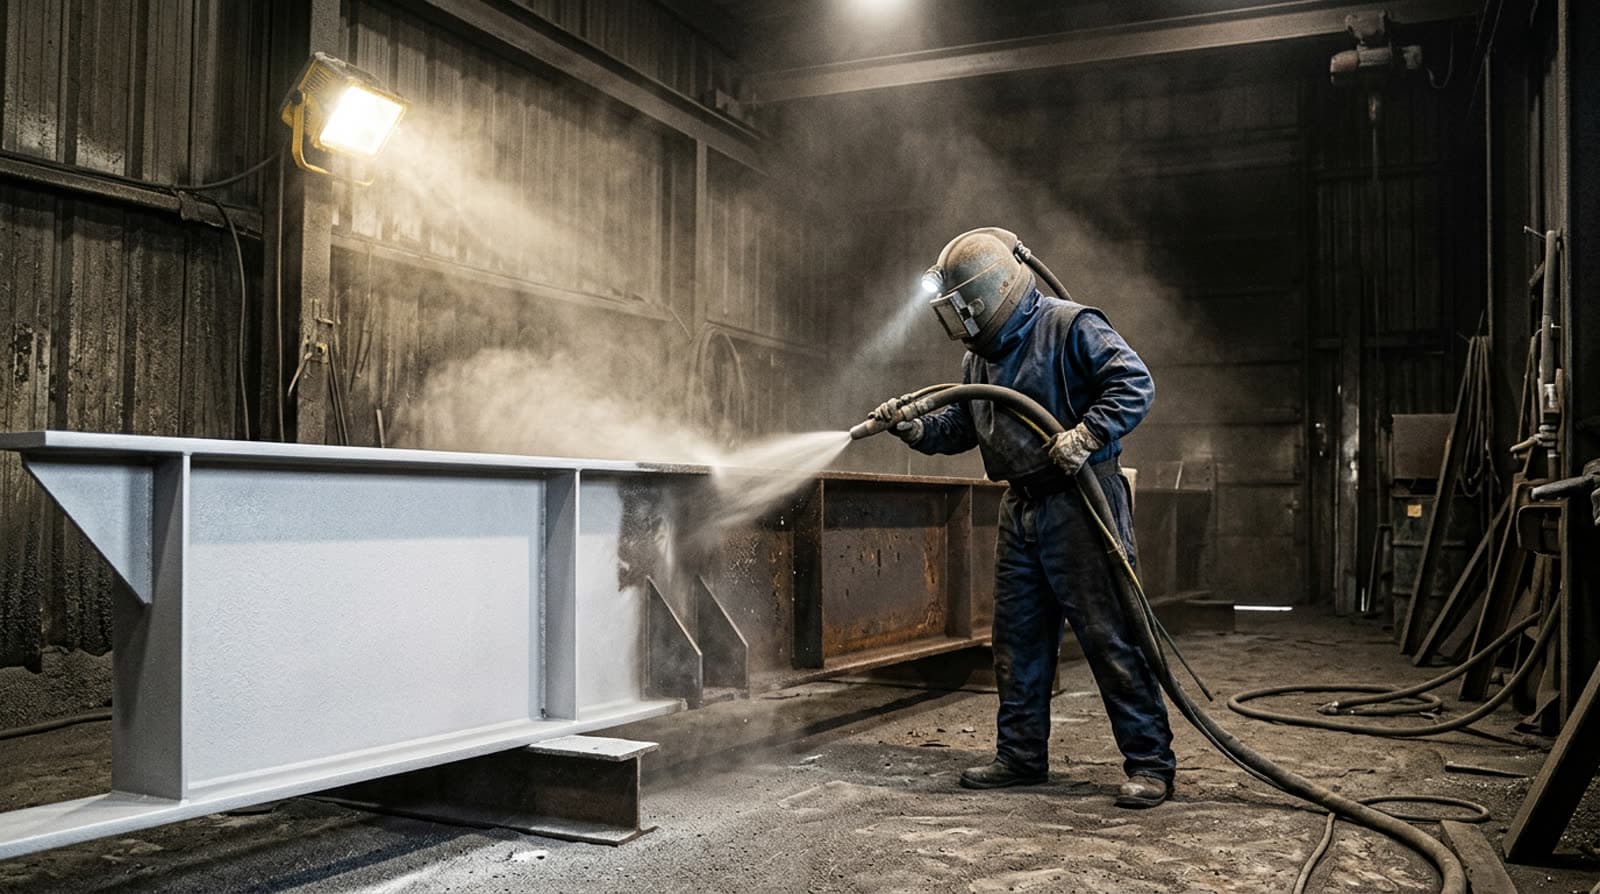
Key takeaways
- Cleanliness grade, surface profile and contamination control are separate requirements; specify each.
- Weld spatter, sharp edges, crevices and weld toes need attention before and after blasting.
- Protect the prepared surface from recontamination and agree on hold points before coating.
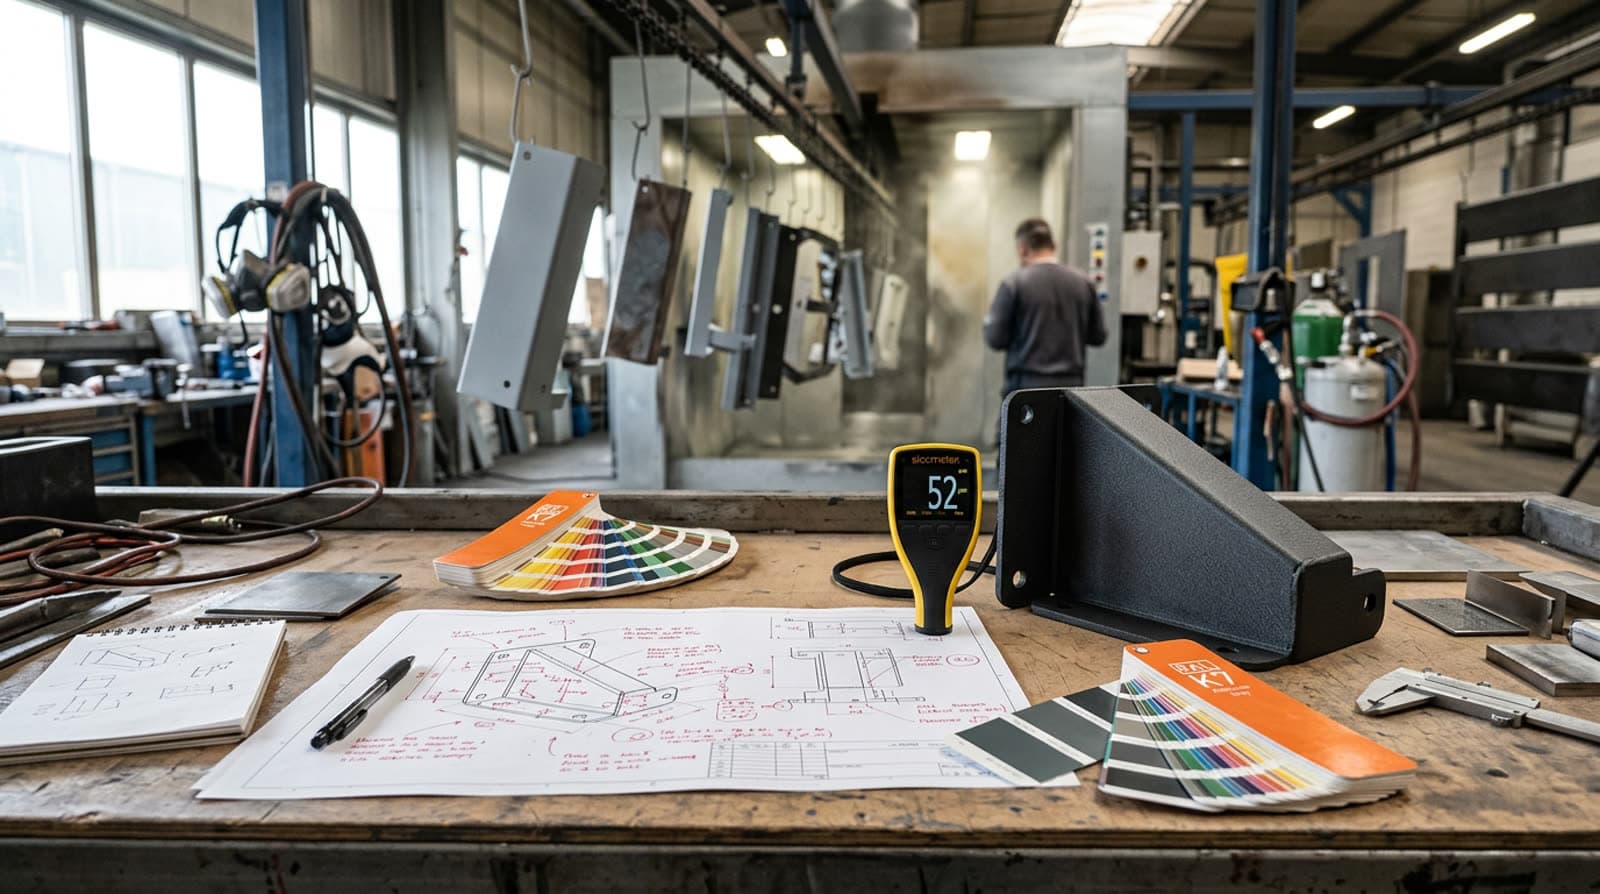
A coating can only bond to the surface actually presented to it. Steel preparation requires decisions about contaminants, rust, mill scale, profile and the interval before coating. The appropriate method depends on the selected system.
Cleanliness and profile are separate requirements
A visual blast-cleaning grade describes the visible condition after preparation. Surface profile describes texture; soluble salts, oil and other contaminants need their own controls. Specify each relevant outcome rather than writing “sandblast” without an acceptance criterion.
AMPP discusses SSPC-SP 10 near-white blast cleaning in the context of certain pipeline coating specifications. That does not make it the universal preparation requirement for all powder coated parts. Follow the coating system and project specification.
- Initial contamination and existing coating
- Required cleanliness grade
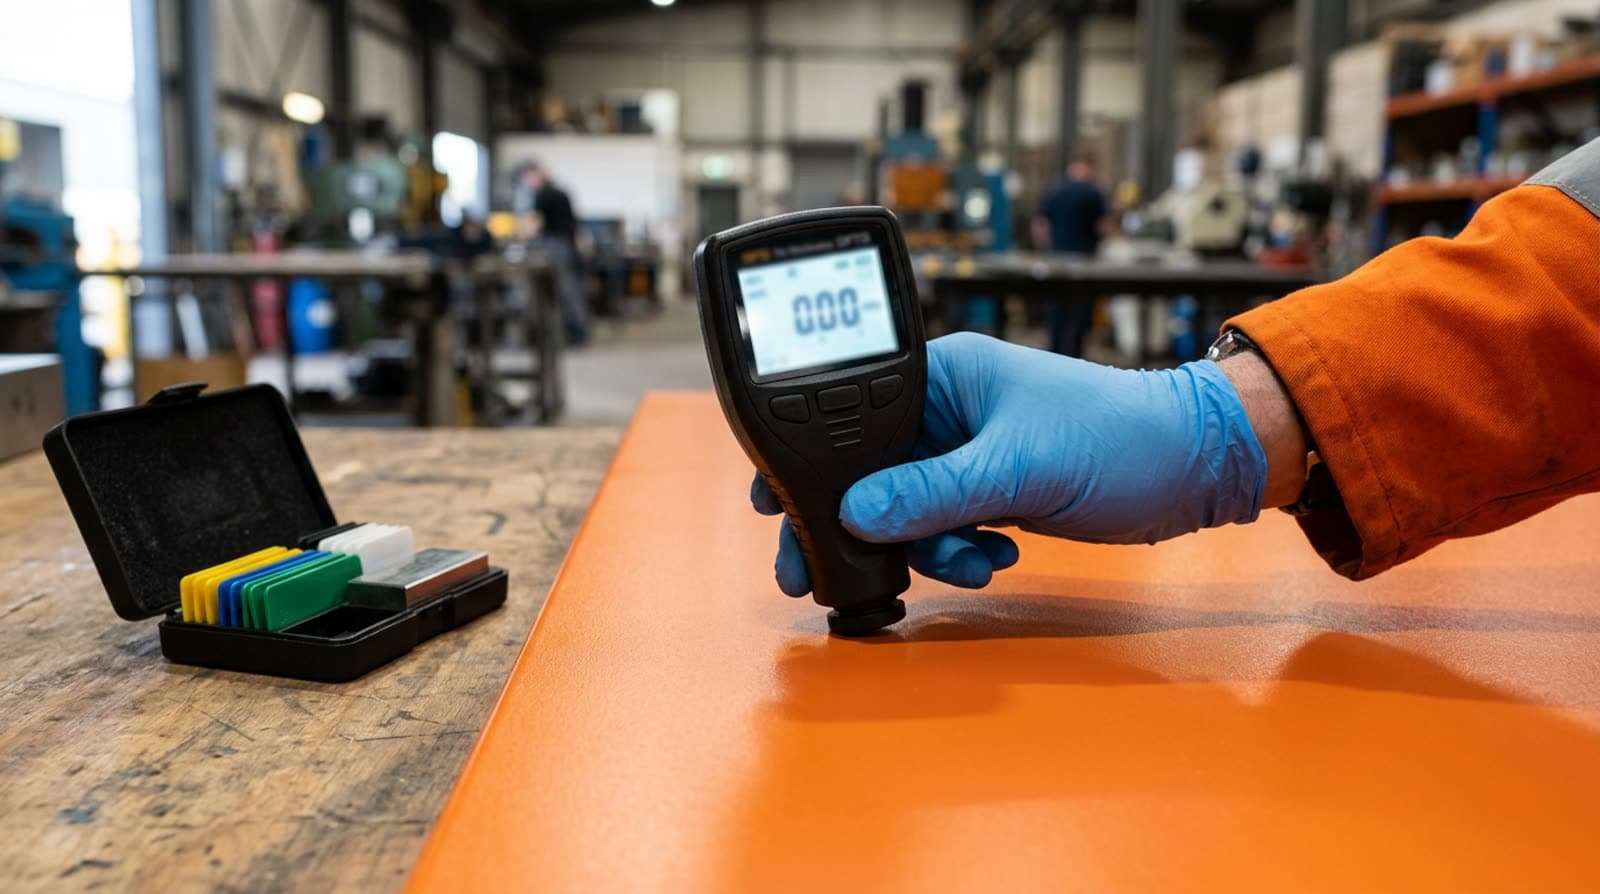
- Profile range and measurement method
- Time and handling before coating
Account for fabrication details
Weld spatter, sharp edges, crevices and heat tint need attention before blasting. A prepared broad face does not prove a tight corner or weld toe is ready. Identify areas that cannot be reached by the chosen abrasive or inspection tool and agree on an alternative.
Abrasive choice should be compatible with the substrate and the specified profile. Record the process for repeat runs so a coating failure can be traced to preparation, application or service damage.
Request the preparation standard, profile range and contamination controls in the same RFQ.
Protect the prepared surface
After blasting, avoid recontamination from handling, moisture and shop debris. Agree on inspection and hold points before primer or powder application. A clean surface can deteriorate if the coating step is delayed or storage conditions change.
Frequently asked questions
Is sandblasting enough of a surface preparation specification?
No. Writing sandblast without criteria leaves cleanliness grade, profile range, measurement method and contamination controls undefined. Specify each outcome.
Is SSPC-SP 10 required for all powder coated steel?
No. SSPC-SP 10 near-white blast cleaning appears in certain pipeline coating specifications, but preparation should follow the selected coating system and project specification.
Why does time between blasting and coating matter?
A prepared surface can deteriorate from handling, moisture and shop debris if coating is delayed or storage conditions change.
Next step
Need blasting and coating under one specification?
Tell us the incoming condition, required cleanliness and profile. We will plan preparation and coating together so nothing falls between the two.
- ISO 9001:2015 registered
- Technical review before pricing
- Toronto facility, North American service